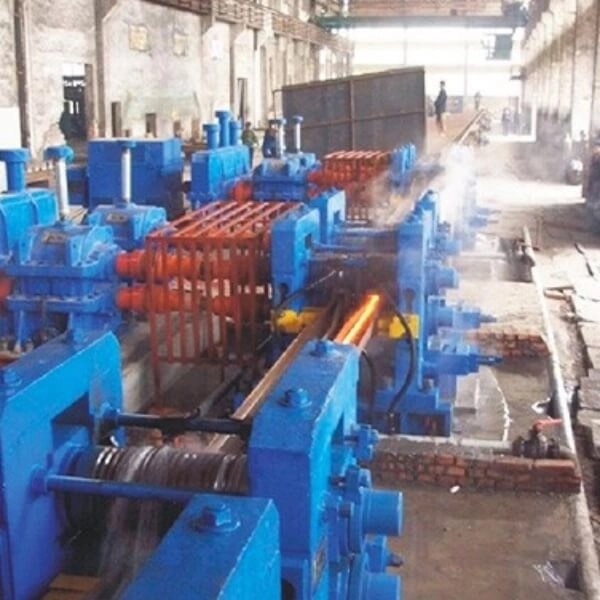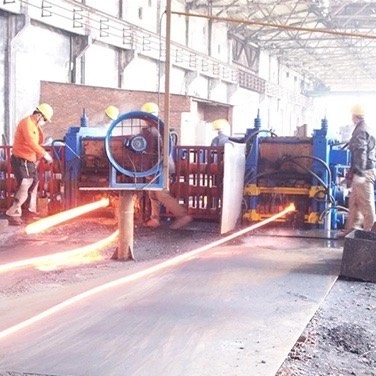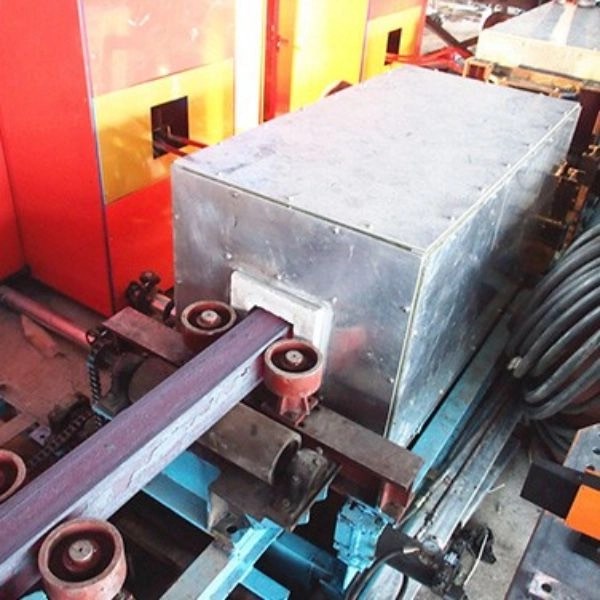
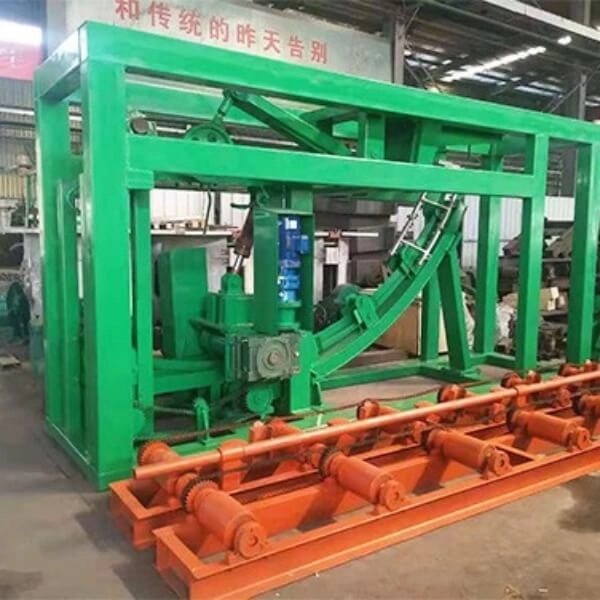
Understand the application.
Output
Convert molten steel into a billet
The caster receives molten steel and forms a solid billet that can be transferred to later processing. Define the steel grade, desired billet section and intended use of the billet. This keeps the casting duty distinct from melting the charge and from rolling the billet into a finished section.
Select the casting-flow and cutting arrangement
The available configuration descriptions distinguish casting flows, billet sections and cutting arrangements. Discuss these as part of one proposed setup. A production figure expressed per flow must remain attached to that flow basis; it should not silently become the output of an entire multi-flow installation or a different billet size.
Plan lifting, cooling and the billet handover
Provide the molten-metal supply arrangement and the way billets will be moved, stored or fed into the next stage. Review workshop lifting space, cooling-water connections and the proposed cutting method alongside the equipment layout. Where a rolling mill is already installed, confirm its accepted billet section and transfer requirements before finalizing the caster interface.
Specifications & configurations.
Technical Specifications
| Main Parameter | R2.25M | R4M | R5.25M | R6M |
|---|---|---|---|---|
| Power | 95KW | 95KW | 95KW | 95KW |
| Billet Size | 60-80 square | 90-150 square | 90-180 square | 90-220 square |
| Flow | One flow or multi-flow according to customer’s requirements | One flow or multi-flow according to customer’s requirements | One flow or multi-flow according to customer’s requirements | One flow or multi-flow according to customer’s requirements |
| Working Speed | Adjustable. Normal working: 4-4.7M/min | Adjustable. Normal working: 4-4.7M/min | Adjustable. Normal working: 4-4.7M/min | Adjustable. Normal working: 4-4.7M/min |
| Cutting Method | Manual / Mechanical / Flame cutting | Manual / Mechanical / Flame cutting | Manual / Mechanical / Flame cutting | Manual / Mechanical / Flame cutting |
| Production Capacity | 4-8T/Hour/ Flow | 8-20T/Hour/Flow | 8-30T/Hour/Flow | 8-50T/Hour/Flow |
| Workshop Lifting height | 6M | 9M | 9-12M | 9-12M |
Before you decide
Does this machine also roll billets into rebar?
Its defined output is a steel billet. Rolling requires a separate receiving stage or a specifically scoped casting-and-rolling line.
How should a per-flow production figure be understood?
Keep it attached to the stated casting flow, billet section and operating conditions. Confirm the combined arrangement before treating it as total plant output.